Laser Welding Production Line for Stainless Steel Tube Optical Fiber Unit


Product Details
1. Introduction
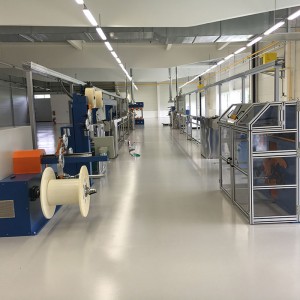
The laser welding production line for stainless steel tube optical fiber unit is used to produce stainless steel tube optical fiber secondary coating units for applications such as OPGW, OPPC,submarine optical cables, etc.
The production line uses laser welding technology to form precision stainless steel tubes from steel strips through forming, welding, and drawing. At the same time, optical fibers and gel are filled into the tubes, resulting in a stainless steel tube optical fiber unit that combines structural strength with transmission performance.
2. Equipment Features
High-precision laser welding keeps the heat-affected zone extremely small, greatly reducing welding deformation and residual stress. This ensures the dimensional accuracy and shape stability of the stainless steel tube.
At the same time, it achieves deep penetration welding, giving the weld high strength and excellent sealing with few defects like porosity or cracks.
Plus, the weld surface is smooth and aesthetic, requiring no post-weld grinding — saving production costs.
3. Main Technical Parameters
| welded diameter of stainless steel tube | φ1.5—φ5.0mm |
| number of optical fibers | Up to 48 fibers (standard configuration) |
| optical fiber pay-off tension | 0.2~1.4N±0.05N |
| excess length range | 1.5‰~3‰ (online) |
| continuous production length | ≥50km |
| optical fiber additional loss | ≤0.01dB/km (G.652D) |
| process welding speed | ≥15 m/min |
Main Components

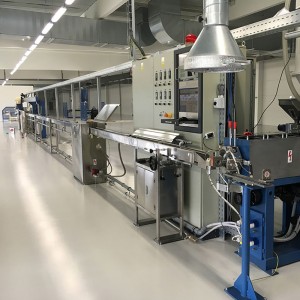
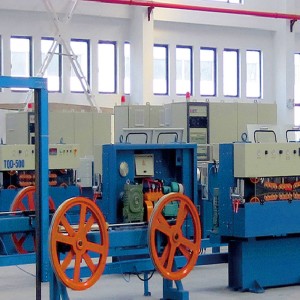
The production line consists of stainless steel strip welding device, stainless steel strip stacking pay-off device, optical fiber pay-off cabinet, stainless steel strip guiding and preparation device, gel filling device, stainless steel strip forming and welding device, stainless steel tube clamping and drawing device, pulling and excess length control device, weld quality monitoring device, take-up device, and electrical control system.
1. Stainless Steel Strip Welding Device
This device is used to pre-splice stainless steel strips end to end to meet the production requirements of long-length stainless steel bundled tubes, and then place them on a stacking pay-off rack.
2. Stainless Steel Strip Stacking Pay-off Device
To meet the requirements of long-length stainless steel tube production, this device uses a stacking structure to connect multiple stainless steel strips in sequence, enabling continuous strip pay-off.
Technical parameters:
Maximum strip storage capacity: 40 km
Maximum number of stacking layers: 10 layers
Two pay-off devices are configured per production line for fast switching.
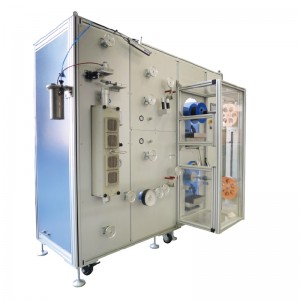
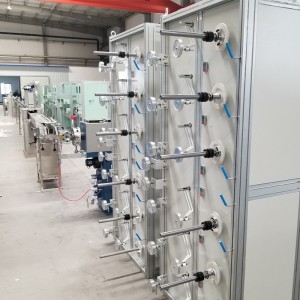
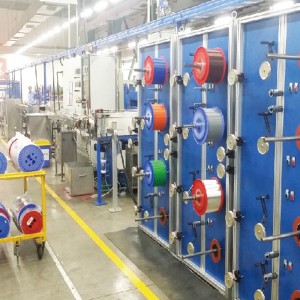
3. 24+24 Optical Fiber Pay-off Cabinet
2 sets of pay-off cabinets provide a total of 48 optical fiber pay-off units, each with digital identification. The combination of an active pay-off design and a dancer-arm tension control system ensures stable fiber pay-off tension.
Cabinet-style structure allows easy integration, compact layout, small footprint, and light weight.
Active pay-off with lever-type dancer-arm tension control, the lever has a scale for direct tension reading.
When fiber breakage occurs, the equipment outputs audible and visual alarms. The fiber spool is not allowed to reverse. The main control panel displays the break and reduces speed to stop the line.
Fiber pay-off and guide devices are equipped with electrostatic dust removal.
The dancer arm and guide wheels are made of lightweight aluminum alloy, with a hard anodized surface finish, and the wheel outer edges are rounded
4. Stainless Steel Strip Guiding and Preparation Device
This unit consists of several components. Its main functions are to clean the stainless steel strip, trim the excess material from both sides of the strip, and ensure that the strip dimensions meet the requirements for welding and forming. After passing through several sets of forming guide rollers, the strip is gradually deformed into the required shape, and then welded by the longitudinal laser welding unit.
5. Gel Filling Device
An A/B tank gel switching device is adopted, with gel being injected from tank B into tank A.
Precision gear pumps are used to inject the gel. The primary gear pump draws the filling gel from the gel tank. The gel then passes through filtration and pressure stabilization, and is delivered by the secondary gear pump through corresponding gel lines into the filling housing. The housing and the associated hoses are equipped with heating elements to ensure that the gel enters the stainless steel tube in a relatively stable state. Meanwhile, the optical fibers converge with the gel and enter the stainless steel tube together.
6. Stainless Steel Strip Longitudinal Forming and Welding Device
The forming device uses multi-stage roller forming, offering high forming speed and stable forming performance.
Longitudinal welding is carried out using laser welding. The welding head is equipped with an optical monitoring channel for the weld spot, enabling automatic tracking of the weld seam and weld spot shape/position, as well as automatic adjustment.
After forming, the stainless steel strip is sized through a sizing die.
7. Stainless Steel Tube Clamping and Drawing Device
Two-stage clamping and two-stage drawing, with the speed ratio of the two drawing stages controlled via a touch screen.
The two-stage gripper-type pulling machine uses grippers to tightly clamp the welded stainless steel tube, preventing the tube from twisting and avoiding any shift in the laser welding point position. At the same time, it provides a certain pulling force to move the steel tube along the production line. The feet of the two-stage gripper pulling machine are equipped with base plates that rest on the ground and are horizontally adjustable.
The drawing device is used to reduce the diameter of the welded stainless steel tube. After passing through the drawing die, the tube diameter decreases from large to small. This not only increases the production speed of the stainless steel tube, but also results in a rounder and smoother outer shape of the drawn tube.
8. Stainless Steel Tube Pulling and Excess Length Control Device
Single-wheel pulling machine (wheel-type pulling): It provides the necessary pulling force for the entire production line, facilitating the stretching of the stainless steel tube. This device is also one of the main components for creating excess length. In addition, a push ring is mounted on the pulling wheel to prevent possible crushing or overlapping between adjacent stainless steel tubes. The base of the single-wheel pulling machine uses an integral flat floor plate that rests on the ground and is horizontally adjustable.
Excess length control device: It controls the speed difference between the single-wheel pulling machine and the downstream gripper-type pulling machine via a tension sensing wheel, causing elastic deformation of the stainless steel tube.
9. Weld Quality Monitoring Device (Eddy Current Flaw Detection)
The welded stainless steel tube passes through the probe of the eddy current flaw detector. If any welding defect is present, the flaw detector will sound an alarm. With the aid of a computer, the signal is displayed on a CRT screen, supporting both memory and real-time display modes. The device features automatic probe matching and is compatible with various types of probes. A German DB eddy current testing device is adopted, which is equipped with a magnetic protection device.
10. Take-up and Traverse Device
The new movable spool traverse design ensures that the stainless steel tube is taken up onto the take-up spool in a straight line, and the traverse pitch is continuously adjustable within a certain range.
The take-up stand has a stable and reliable overall structure. When the full spool is present and the stop button is pressed, the take-up stand stops quickly, with the inertial rotation not exceeding one revolution.
11. Electrical Control System
The entire production line adopts an industrial PC and a Siemens S7 control system. Major production line operations and process parameter settings are carried out via the industrial PC and Siemens S7 controller, which also supports production information management (data logging) and process parameter management (recipe management).
Data exchange between the various PLCs on the production line is conducted through the Profibus fieldbus, enabling full-line machine control.
Motors, frequency converters, low-voltage electrical components, etc., are sourced from international top-tier brands such as Siemens, Schneider, and Danfoss.
A chassis is installed at the bottom of the electrical control cabinet. Internal wiring follows Siemens standards, and the power supply is wired according to the three-phase five-wire system. All grounding wires and equipment enclosures are reliably grounded.
FAQ
Q: Can I visit your factory?
A: All the customers from both home and abroad are warmly welcomed to visit our company and factory.
Q: Do you supply the installation and commissioning?
A: Yes, we do as followings:
-As soon as customer informed us the machines are put in the right place, we will send both mechanical and electrical engineer for machine start up.
-No-load testing: After machine installed completely, we make no-load testing first.
-With-load testing: Usually we will can produce 3 different wires to make load testing.
-Acceptance report: After the buyer confirms that machine can reach all specification under contract, the acceptance report will be signed for our record that machine will be in guarantee period.
Q: What information should I offer to get a detailed quotation from you?
A: For single machine: Usually we need to know inlet wire size, outlet wire size to be produced, productivity, pay off and take up size to choose the right machine.
For new cable plant or new cable production line, we need to know the datasheet of cables to be produced, the productivity, the standards to be followed, etc to design all machines needed.
Q: Can you supply the auxiliary equipment along with the machines?
A: Yes, definitely.
We has supplied heat exchanger, copper/aluminum powder filter machine, cooling tower, chiller, air compressor, drawing dies, pointing machine, cold welders, bobbins etc. with our machines.
Q: Could you do the design for the whole plant?
A: Yes, this is our advantage.
With the data sheet of cable to be produced, the standard your cables should follows, the productivity you expected. Our engineer on production technology and machinery will make design of production machines, test equipment, accessories like bobbins, dies, rewinding lines and materials needed.
Q: How can I know the status of my order?
A: We have our OA system on tracking the production.
For any of your request we can send photos and videos of your order, also we can use FACETIME to let you know the production.
Q: How do you work on the inspection before delivery?
A: We will make dynamic balance testing, levelness testing, noise testing, etc. during production.
After production finished, usually we make no-load running of each machine before delivery. Customers are welcomed to attend the inspection.
Q: What exhibitions will you attend, can we meet in the fair?
A: Dusseldorf International Wire and Cable Fair;
Wire South America Fair;
International Wire and Cable Fair in Shanghai;
International Istanbul Wire Fair, etc.
wire Southeast Asia Fair, etc.